
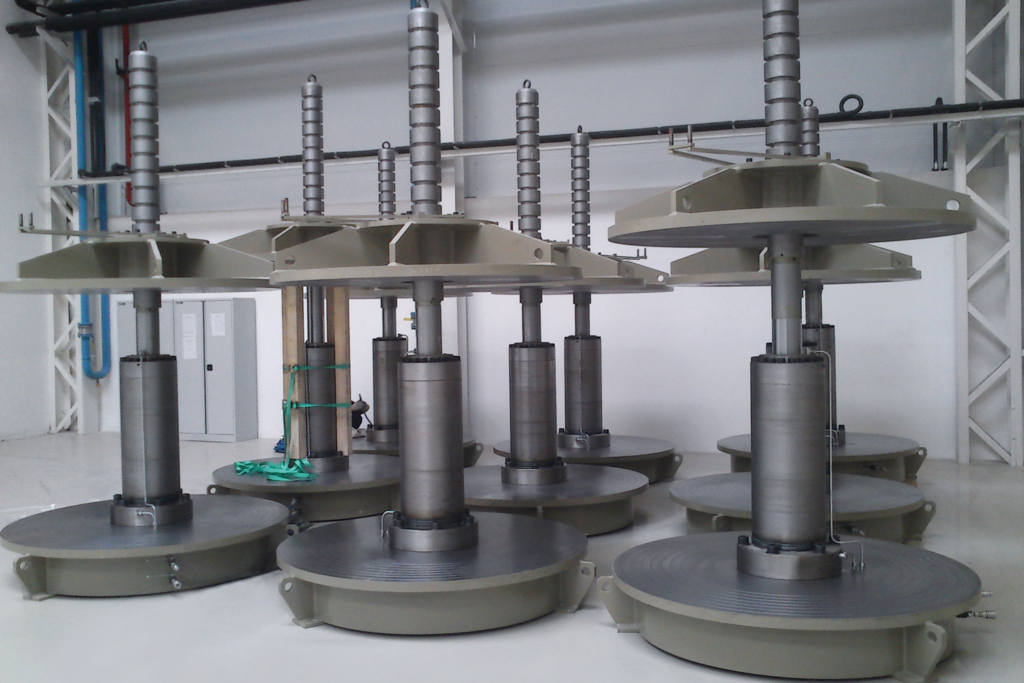
What Is Isostatic Pressing?
Isostatic pressing is a manufacturing process that applies pressure from all directions to compact powders or densify suitable components. Cold isostatic pressing (CIP) usually compacts powder inside a flexible mold using liquid pressure. Warm isostatic pressing (WIP) adds controlled heating to a liquid-pressure process. Hot isostatic pressing (HIP) combines elevated temperature with gas pressure to consolidate material or reduce suitable internal porosity.
The main benefit is more uniform compaction or improved density not a guarantee of identical wall thickness, zero shrinkage or a finished part that needs no machining. The appropriate process depends on the starting material, component geometry and required final properties.
Explore the comprehensive guide to isostatic pressing, a key powder compaction technique. Learn about its cycle, types (CIP, WIP, HIP), advantages, applications across industries, and design considerations for crafting dense and uniform parts.
Understanding Isostatic Pressing: Crafting Dense and Uniform Parts

This article covers a comprehensive overview of isostatic pressing, including its principles and the comparison between wet sack and dry pack methods. It delves into the three main types: Cold Isostatic Pressing (CIP), Warm Pressing (WIP), and Hot Pressing (HIP). The advantages of pressing are highlighted, focusing on uniform part thickness, improved material properties, reduce CNC machining costs needs, and design flexibility. Applications across various industries are discussed, along with detailed procedures for each type of pressing.
Key design considerations, such as container materials, weld positioning, tolerances, and computer modeling, are explored. The article also addresses post-processing techniques, including heat treatment, machining, and surface treatment.
Isostatic pressing is a powder compaction strategy that takes into consideration making of uniform thickness parts. This article examines the cycle, types, benefits, applications, plan viewpoints and more to give an exhaustive comprehension of pressing.
Technical clarification: In this context, uniformity refers primarily to the applied pressure and the resulting compaction or density distribution. Wall thickness is a design dimension. A part can have different wall thicknesses while still benefiting from isostatic pressure. Shrinkage and dimensional changes must be allowed for rather than assumed to be insignificant.
Isostatic Pressing Cycle

The pressing cycle depends on whether the goal is to form a powder compact or densify an existing component. Preparation establishes the material, tooling or capsule, and approved processing conditions. The equipment then applies pressure, holds the specified conditions and releases them through a controlled sequence. Heated processes also require a suitable cooling stage before unloading.
For a powder route, pressing may be only one stage of production. Subsequent sintering, heat treatment, machining and inspection can determine whether the component meets its final requirements.
Standards of Isostatic Pressing
Isostatic pressing uses liquid strain to minimized powder inside an adaptable form. Powders are set in a form and exposed to rise to strain from all bearings utilizing a fluid or gas, molding them consistently.
More precisely, the surrounding pressure medium transmits pressure around the workpiece or its container. CIP commonly uses liquid around a flexible mold. HIP generally uses high-pressure gas in a heated pressure vessel; its tooling and preparation are therefore different from those of CIP. Uniform external pressure does not remove the need to control powder packing, mold behavior or the material’s response.
Wet Sack vs Dry Pack Methods
The wet sack strategy includes lowering powder-filled adaptable packs in a high pressure die casting liquid. The dry pack fixes the sack inside the vessel, permitting powder stacking without expulsion.
Terminology clarification: The standard names are wet-bag pressing and dry-bag pressing. In wet-bag pressing, the filled flexible mold is immersed in the pressure liquid and removed after the cycle. In dry-bag pressing, the flexible tooling remains installed in the equipment while material is loaded and the compact is removed. The distinction concerns the tooling arrangement, not whether powder is intentionally mixed with the pressure liquid.
Isostatic powder compaction is also different from high-pressure die casting. In the CIP process described by Quintus, powder is enclosed in a flexible mold and compacted by the surrounding pressure medium; it is not injected into a die as molten metal.
Kinds of Isostatic Pressing: CIP, WIP, HIP

Isostatic pressing happens at various temperatures – cold (<100°C), warm (<boiling point) or hot (up to 2200°C) – delegated CIP, WIP and HIP individually.
Temperature clarification: The values above should not be used as universal process boundaries or as operating instructions. CIP, WIP and HIP differ in their processing purpose, temperature and pressure medium. WIP uses a heated, pressurized liquid; its allowable temperature depends on the selected medium and equipment, not a single normal-boiling-point rule. HIP conditions are selected for the material and qualified cycle, so an equipment maximum is not automatically an appropriate processing temperature.
Choosing between the three: Consider CIP when the immediate objective is a powder compact that will undergo further processing. Consider WIP when controlled heating helps the material’s compaction or consolidation behavior. Consider HIP when the objective is high-temperature consolidation or the reduction of suitable internal porosity. The process provider should confirm suitability rather than choosing solely from a temperature label.
Advantages of Isostatic Pressing
- Uniform Part Thickness: Applying equivalent tension gives reliably thick parts insignificant shrinkage and disfigurement.
- Worked on Material Properties: The fine, homogeneous microstructures confer strength values like fashioned metals.
- Diminished Machining Needs: Close endlessly net shapes limit post-handling for complex clay or metal parts.
- Plan Adaptability: Complex undermines, long/slender calculations and bimetal developments are conceivable.
Important limits to these advantages: More uniform pressure can support consistent compaction, but it does not guarantee uniform dimensions or eliminate distortion. Changes in microstructure and mechanical properties depend on the material and processing cycle; properties equivalent to a forged product should not be assumed without qualification.
Near-net-shape production may reduce the material that must be removed later, but precision faces, holes, threads and fits can still require machining. Design freedom also remains subject to tooling removal, capsule manufacture, material compatibility and inspection access. A complex shape is not automatically feasible simply because pressure acts from all directions.
Uses of Isostatic Pressing
- Powder Compaction and Clay Handling: CIP compacts ceramics like alumina, working on mechanical properties for enterprises.
- Metal Powders and Composite Materials: CIP/HIP cycles prepares, superalloys and tungsten powders into leaves behind applications in different areas.
- Enterprises Using Isostatic Pressing: Aviation, auto, energy, clinical, atomic and more influence uniform thickness and plan opportunity.
CIP applications focus on preparing powder compacts for further processing. HIP can serve a different role: improving the density of suitable castings, powder-derived components and metal additive-manufactured parts. Bodycote identifies HIP as a way to address internal porosity in applicable materials and manufacturing routes.
For example, a ceramic powder body may be cold-isostatically pressed before sintering, while a suitable metal casting may undergo HIP after casting. These routes have different starting conditions and acceptance criteria. Listing an industry or material does not establish that every component in that category is suitable for the process or approved for service.
Isostatic Pressing Procedures

- Cold Isostatic Pressing (CIP): CIP compacts powders into adaptable molds lowered in liquid at room temperature.
- CIP Interaction: Powders are stacked into fixed adaptable packs and exposed to approach hydrostatic tension.
- Materials Utilized in CIP: CIP processes different earthenware production and metals like compounds and tungsten.
A typical CIP powder route involves preparing and filling the flexible mold, compacting the powder under liquid pressure, releasing the pressure and carefully removing the compact. The result is commonly called a green compact: it has been formed but normally still requires sintering or another densification stage before it has the intended final material properties.
Powder consistency, filling, mold design and handling therefore matter alongside the selected pressing conditions. Define the required final density, dimensions and material properties separately from the requirements for the pressed compact.
Warm Isostatic Pressing (WIP)
- WIP Cycle: WIP uses warmed fluid media to apply uniform tension underneath the medium’s edge of boiling over.
- Ventures Utilizing WIP: Hardware, plastics and covers influence controlled compaction at exact temperatures.
WIP is best understood as compaction or consolidation using a heated, pressurized liquid medium. Temperature control is part of the process specification, alongside pressure and holding conditions. The medium, tooling and material must remain compatible throughout the cycle.
Clarification: WIP should not be defined as universally operating below the liquid’s normal boiling point. The process uses pressurized equipment, and the approved operating conditions depend on that system. For a project, ask what the warm process is intended to improve and how that result will be measured; the presence of heat alone does not establish suitability.
Hot Isostatic Pressing (HIP)
- HIP Cycle: HIP densifies materials at the same time under high temperature and tension in an idle air.
- Advantages of HIP: HIP kills surrenders and isotopically improves properties for designing pottery.
- Technical clarification: HIP uses elevated temperature and isostatic gas pressure, commonly with an inert gas. Powder consolidation typically requires a gas-tight capsule. An existing casting or additive-manufactured component has a different preparation route and must meet the process provider’s suitability requirements.
HIP can reduce suitable internal pores, but it does not guarantee the removal of every defect. Surface-connected porosity is a key limitation: gas can reach the pore surfaces, so the pore does not experience the same closing action as a sealed internal void. Do not assume that every crack or lack-of-fusion defect will disappear.
The phrase “isotopically improves” above should be read as a reference to potential improvements in material properties, not to changes in isotopes. HIP does not automatically prove isotropic behavior, a specified strength or compliance with an application standard. Agree the target properties and inspection evidence before processing.
Plan Contemplations for Isostatic Pressing
- Holder Materials and Shrinkage: Steel or titanium holders shrivel non-consistently relying upon calculation and welds.
- Situating of Holder Welds: Welds situated internal or outward influence disfigurement, with internal welds liked.
- Resistances for Isostatic Parts: Resistances rely upon different elements like calculation, materials and chain boundaries.
- PC Displaying: Reenactment advances processes for complex shapes by anticipating shrinkage and densities.
Here, the practical design concerns are container or capsule design, shrinkage allowance, final tolerances and process simulation. For powder HIP, the capsule must provide a suitable gas-tight enclosure. Its geometry and material response must be considered together with the powder and intended component.
Weld clarification: The retained statement about inward welds should not be treated as a universal design rule. Weld positioning, leak integrity and distortion require component-specific assessment. Likewise, naming steel or titanium as a container material is not enough to establish compatibility or predictable shrinkage.
Specify the final drawing separately from any intermediate pressing geometry. Identify critical datums, sealing faces, fits and inspection surfaces, and decide which will be finished after densification. Process simulation can help plan deformation, but it does not replace dimensional inspection or an approved production trial. Bodycote’s HIP guidance also makes clear that distortion considerations depend on the component and material condition.
Post-Handling of Isostatic Parts
- Heat Treatment: HIP empowers heat treatment solidification for mechanical property improvement.
- Machining: Optional cycles like CNC machining refine close net shapes to practical resiliences.
- Surface Treatment: Plating, covering and completing safeguard surfaces and further develop usefulness.
The post-processing route should establish the delivered material condition, not merely whether the part has been pressed. Depending on the component, that route may include sintering, capsule removal, heat treatment, machining, surface finishing and inspection. HIP equipment can integrate certain heat-treatment operations, but this does not automatically replace every treatment required by the material specification.
For critical interfaces, CNC machining services can be considered after densification, subject to material and component feasibility. Define the machining allowance, final dimensions, surface requirements and inspection plan before requesting pricing. Avoid assuming that a near-net-shape pressed part is already within its final tolerances.
Use MXY’s CNC machining RFQ checklist to communicate the controlled drawing, exact material grade and condition, quantity, finishing and acceptance requirements. Confirm which operations are available for the specific component; this article does not establish that MXY provides in-house CIP, WIP or HIP.
Conclusion
In conclusion, isostatic pressing is a flexible powder compaction strategy that has essentially influenced fabricating processes across various enterprises. By applying uniform pressure from every direction, isostatic pressing helps produce parts with more consistent density and fewer compaction-related defects. This has empowered creation of intricate parts that were already difficult to make through ordinary strategies.
Whether it is chilly, warm or hot pressing, every variation offers unmistakable benefits in view of the temperature control and material being handled. With headways in PC displaying, holder plan, and cycle robotization, more tight resiliences and higher cycle throughput have been attainable. As inventive material details and added substance producing keep on arising, the adaptability of pressing guarantees its significance as a proficient densification arrangement. Going ahead, further interaction enhancement will grow the achievable applications extent of this basic powder compaction innovation.
FAQs
Q: What is the standard behind isostatic pressing?
A: Pressure is applied from all directions through the surrounding medium. For CIP, liquid pressure acts around a flexible powder-filled mold. For HIP, heated gas pressure acts on a suitably prepared component or gas-tight powder capsule. Uniform applied pressure should not be confused with automatically uniform final wall thickness.
Q: What are the fundamental sorts of isostatic pressing?
A: The full names are cold isostatic pressing, warm isostatic pressing and hot isostatic pressing. The temperature statements in the original answer are broad descriptions, not universal equipment limits or material processing instructions. WIP is defined by heated liquid-pressure processing; HIP uses elevated temperature and gas pressure. Select the actual cycle with the process provider.
Q: What materials can be handled utilizing isostatic pressing?
A: Suitability depends on the exact material, starting condition and processing route. Powder compaction by CIP does not by itself establish final density or mechanical properties; further processing is normally needed. HIP is also used for suitable existing components, not only loose powder. Confirm the required final condition and qualification evidence rather than treating a material family as approval for every application.
Q: What are the normal uses of isostatic pressing?
A: These examples describe application areas, not a guarantee that every part in those areas should be isostatically pressed. The process must fit the component’s material, geometry, defect state and acceptance requirements. In particular, HIP treatment of a metal additive-manufactured component is a post-processing decision, not proof that all printing defects have been removed.
Q: Does cold isostatic pressing replace sintering?
No. CIP normally forms a green compact. Sintering or another appropriate densification step is generally still needed to develop the required final density and properties. Plan the full route rather than accepting the pressed shape as a finished component.
Q: Can hot isostatic pressing remove all porosity?
No. HIP can reduce suitable internal porosity, but surface-connected pores are a known limitation. Material condition and the qualified cycle also matter. Agree the defect acceptance criteria and inspection method before treatment.
Q: Will an isostatically pressed part still need CNC machining?
It may. Near-net-shape production can reduce the material left for machining, but critical fits, threads, datum surfaces and finishes may still need secondary operations. Define the final drawing requirements and confirm machining feasibility for the actual material and component.


